

Line 2 · end of shift
The supervisor writes down how many parts came out and someone enters them the next day. The machine was already counting, but that data never leaves it.
We read what your machines already record and take it to a screen above the line, the quality report and the company system. We build what your plant needs, from a production board to camera inspection, without touching line control, and we improve the operation around it: supply, warehousing, inventory, planning and shipping.
Line 2 · end of shift
The supervisor writes down how many parts came out and someone enters them the next day. The machine was already counting, but that data never leaves it.
Maintenance · machine stop
The machine stops and nobody knows how long it was down until someone walks by. At month end there is no way to know which stops cost the most.
Quality · customer audit
The customer asks for the oven temperature or a photo of a part from a lot made weeks ago, and someone searches printed sheets.
What can be built from the data your plant already produces. Three of these projects have their own page.
Parts, stops and speed from each machine, read from your PLCs and sensors and stored by shift, lot and part number.
See industrial automationTarget versus actual hour by hour, stops with their cause and the shift's OEE on a screen above each line and on the manager's phone.
See visual factoryA camera checks every part, sets aside the bad one and keeps the photo of each reject with time and lot.
See machine visionRejects, process parameters and photos tied to the lot and part number, so an audit is answered with the lot number in hand.
Stop alerts as they happen, failure history per machine and preventive maintenance scheduled by usage hours.
Raw material and finished goods inventory, line-side replenishment, purchase orders and the production plan, built on what is actually in the warehouse. We review with your team how it is done today and change the operation, not only the system.
Production and stops ready at shift change, and an agent that drafts the summary for the morning meeting.
If your plant needs something that is not here, we build that too: the record of an inspection done on paper today, the connection to your quality system or an app for the raw material warehouse. The one thing we leave out is electrical work: we do not build electrical panels or program PLCs.
Book a callEach key on the plan leads to its page. The blue line is the work almost nobody does: taking what happens on the plant floor into the office system, and back.
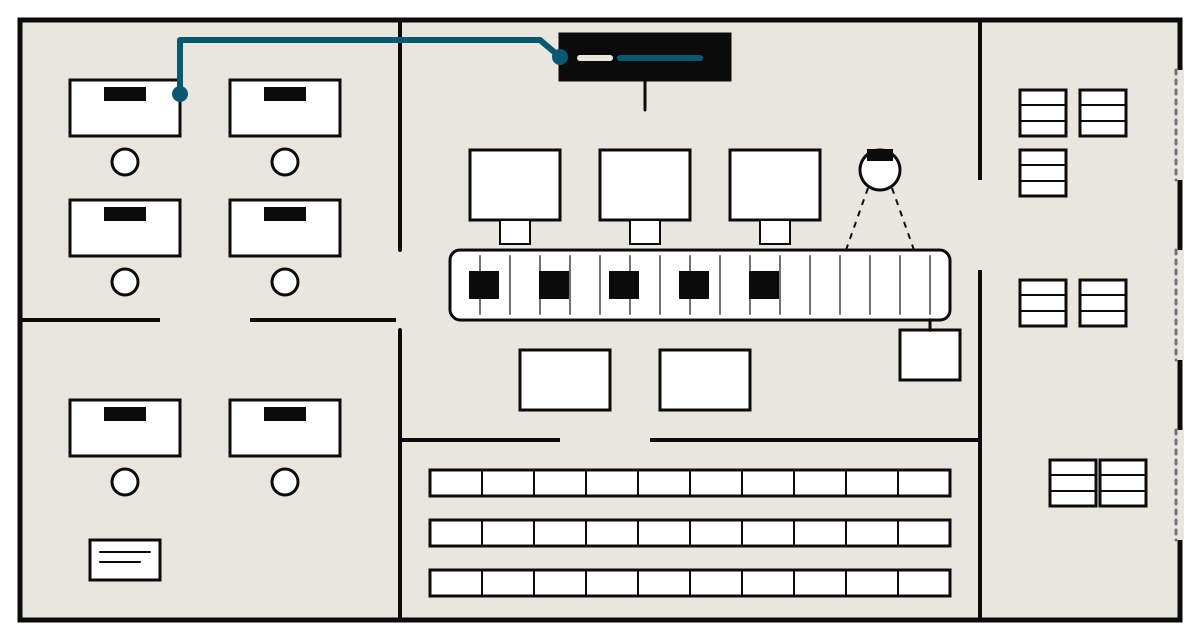
What your machines record, in the company system.
We read what your machines already record and take it to the shift's production, the quality report and the company system, without touching line control.
Target, actual and stops, hour by hour.
A screen above each line with the target, the actual count and why it stopped, hour by hour. The supervisor no longer walks the floor to fill in the whiteboard.
A camera checks and counts every part.
A camera checks every part that goes by, counts by part number and sets aside the bad one. Every reject leaves a photo with time and lot.
We work with the PLCs, sensors, cameras and screens already in your plant, whatever the brand. If a machine does not store the data needed, we propose the equipment required and explain why.
We visit the plant and review with your team what each machine records. We set up a parallel trial on one line, without touching its program, and compare what we read with what the supervisor writes down today. With your approval we move on to the others.
It depends on how many machines and lines there are, how different they are from each other and whether a sensor, camera or screen has to be added. After the visit we send the scope, price and dates in writing.
How we work: scope, deliveries and maintenanceWe do not have a published plant case yet. What you can see before deciding: during the visit we review your machines with your maintenance team, and in the parallel trial you compare what we read with what your supervisor writes down today, with your own production.
No. The trial runs in parallel and only reads data. It is connected to the line once the plant approves it, at a time the plant chooses.
No. We read what the machine already records and line control stays as it is. We do not program PLCs or build electrical panels; if a machine needs a change, your maintenance team or your integrator makes it.
We read the PLCs and use the cameras already in your plant, whatever the brand. If equipment is missing, we propose what is needed and explain why.
The same team that installed it. We answer every day, and the system alerts when it stops receiving data from a machine.
No. It starts with one line or one machine and expands once the plant sees the result.
We visit the plant, review what your machines record and tell you what can be read and taken into the company system.
Documents: Privacy notice · Terms of use